When I first started fielding questions from medical device manufacturers about our capping machines, I’ll admit I didn’t expect the line of inquiry to center so heavily on regulatory compliance. For 12 years, I’ve been the face of a capping machine supplier—you know, the guy who flies out to a client’s factory at 2 a.m. to troubleshoot a misfilling cap on a vial of diagnostic reagent, or stays up until 3 a.m. calibrating a machine for a client packaging insulin pens. But over the past three years, this question has gotten so frequent that I’ve started carrying a one-page quick-reference sheet in my laptop bag: “Can a capping machine be used for medical device packaging?” It’s not a yes or no answer, really—it’s a “how, and under what conditions” answer, and if you’re someone who’s juggling FDA guidelines, ISO 13485 audits, and the pressure to get a new product to market 12 months early, that distinction matters more than you might think. Capping Machine
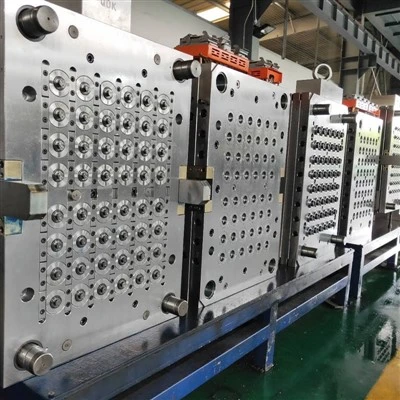
Let me start with the basics: what is medical device packaging, exactly? It’s not just slapping a lid on a bottle and calling it done. Medical devices range from implantable pacemaker leads that need to stay sterile for 10 years to single-use syringes that require tamper-evident seals to over-the-counter blood glucose test strips that need to stay moisture-free for two years. Each of these has specific requirements for seal integrity, sterility, material compatibility, and traceability—and that’s where a standard capping machine (the kind that’s used for, say, food or cosmetic products) falls short. But here’s the good news: most of our clients don’t need to buy a brand-new, custom-built machine from scratch. They just need to adapt the capping technology they already rely on for other products to meet medical standards, and that’s a service we specialize in.
I’ll give you a recent example that still gives me flashbacks. Last year, a small biotech startup out of Boston called me panicking. They’d developed a new portable nebulizer for pediatric asthma patients, and their original capping machine—something they’d used to package cleaning supplies for their lab—was failing a critical seal integrity test. The cap was a small, overmolded rubber seal that needed to create hermetic pressure to keep the medication inside sterile, but their old machine was applying too much torque, warping the seal, or too little, letting air seep in. The startup was three weeks away from a scheduled FDA pre-submission, and their entire budget was tied up in clinical trial costs.
I hopped on a red-eye to Logan, and by the time I got to their facility at 7 a.m., I’d already pulled their cap specs, the FDA’s guidance on medical device packaging sealing, and our machine’s calibration data onto my tablet. The problem wasn’t that their capping machine was a “non-medical” machine—it was that it was calibrated for plastic water bottles, not precision rubber seals. We swapped out the standard torque head on our semi-automatic capper for a low-torque, precision-controlled head that allowed incremental adjustments down to 0.1 Nm (that’s a unit of torque, if you’re not familiar, and for reference, food cappers usually adjust in 0.5 Nm increments at best). We also added a leak test module—something most standard cappers skip—that uses vacuum decay to check for micro-leaks in real time, so every cap that went on a nebulizer was tested before it left the line.
We ran a 24-hour test batch that same week, and not a single seal failed the integrity check. That client is now scaling to 100,000 units a month, and they still use our capping machines exclusively for their product line. But here’s the part most people don’t hear: we didn’t reinvent the wheel for them. We just modified the capping machine they already trusted, because medical device packaging doesn’t require entirely new technology—it requires that technology to meet specific, strict standards.
Let’s break down the key requirements that separate a standard capping machine from one that’s suitable for medical device packaging, because that’s where the confusion comes from. First is material compatibility. Medical devices often use sensitive materials: silicone, rubber, plastic resins like polycarbonate or cyclic olefin copolymer, even metals like titanium. A standard capping machine uses aluminum or steel components that can leach micro-particulates onto your packaging or your device, which is a big no-no for products that come into contact with bodily fluids or are inserted into the body. For example, if you’re packaging implantable insulin pumps, a tiny piece of aluminum from a worn capper component could get trapped in the seal, leading to inflammation in a patient’s body. That’s why all the components of medical-grade cappers need to be made of 316L stainless steel or medical-grade plastic—materials that are non-leaching and easy to sterilize between runs.
Second is process validation. This is the part that gives operations managers nightmares, but it’s non-negotiable for medical devices. The FDA and ISO 13485 require that every step of your packaging process is validated to show it consistently does what it’s supposed to. A standard capper can’t tell you that a cap is seated correctly—you have to stop the line and check every few hours, which is slow and risky. A medical capper, on the other hand, uses real-time monitoring systems: torque sensors that log every cap’s tightness, vision systems that check for misaligned caps or damaged seals, and even traceability tags that link each package to a production batch. That means if you ever have to do a recall, you can track exactly which units were made on which day, on which machine, and even which operator ran the line. For standard food or cosmetic products, that level of traceability is nice to have, but for medical devices, it’s legally required.
Third is sterility assurance. If your medical device is a sterile product—like a surgical instrument, a vial of injectable medication, or a single-use catheter—your packaging has to stay sterile until the end user opens it. A standard capper isn’t designed for use in a cleanroom. It might have gaps where dust or microbes can get trapped, and it can’t be sterilized with the same processes used for medical equipment. Medical-grade cappers, though, are built to meet ISO Class 7 or Class 8 cleanroom standards (the most common for medical device assembly). They have sealed, crevice-free components that can be fully sanitized with gamma irradiation, ethylene oxide, or hydrogen peroxide vapor, and they’re designed to run without generating dust or particulates that could contaminate a sterile product.
But wait—does that mean every capping machine can be modified for medical use? Absolutely not. There are a lot of machines out there that look like medical cappers on the outside, but they’re just standard cappers with a new paint job and a few extra sensors, and they’ll fail an audit every single time. The key is working with a supplier who understands both capping technology and medical regulations. For example, we don’t sell a “one-size-fits-all” medical capper. We walk through every client’s needs with them: what type of device are they packaging? Is it sterile or non-sterile? What are their throughput requirements? What regulatory bodies do they need to comply with (FDA, CE, Health Canada, etc.)? Then we modify our standard capping models to meet those specific requirements.
Take another example: a client that manufactures single-use insulin pens. Their product isn’t sterile until it’s sealed in its blister pack, but the cap itself has to be tamper-evident, and it can’t be so tight that a patient with arthritis can’t open it. That’s a tricky balance. Our standard automatic inline capper was already capable of high throughput—up to 60 units per minute—but we modified it to include a dynamic torque system that adjusts based on the cap’s material and size, and we added a tamper-evident seal verification that uses a camera to check that the seal is intact after capping. We also worked with their quality team to create a process validation protocol that’s fully compliant with 21 CFR Part 820, the FDA’s regulation for medical device quality systems. Now that client produces 500,000 insulin pens a month, and they’ve passed three consecutive audits with zero non-conformances.
I know a lot of people reading this might be thinking: “Why not just buy a custom medical capper from the start?” The answer is cost. Custom-built machines can cost 2-3 times more than a modified standard capper, and they have longer lead times. For small startups or mid-sized manufacturers, that’s a huge barrier. For example, a custom medical capper can cost upwards of $200,000, while a modified semi-automatic or inline capper from us is often under $100,000, with a lead time of 4-6 weeks instead of 6 months. That’s a game-changer for companies that are trying to get a new medical device to market quickly without breaking the bank.
But there are pitfalls to watch out for when you’re adapting a capping machine for medical use, and I’ve seen clients make every single one of them. The first mistake is skimping on validation. A lot of operators will say, “Well, this machine worked for our other products, so it should work for this medical device.” But that’s not how regulatory compliance works. Every new product, every new line, even every new batch of caps, needs to be re-validated. I had a client a few years ago who skipped the validation step because they were in a hurry, and they got an FDA Form 483 (a notice of objection) during their audit because their seal integrity data didn’t prove consistency. It set their launch back 6 months, cost them millions in delayed revenue, and almost put them out of business. Lesson learned: validation isn’t optional for medical devices.
The second mistake is ignoring material traceability. Standard cappers often use generic components that aren’t tracked, but for medical use, every part of your machine that comes into contact with your packaging or device needs to be traceable. That way, if a component wears out or causes a problem, you can track exactly when it was installed, what material it’s made of, and whether it meets medical standards. We keep a full material history for every capping machine we sell, so our clients can provide that documentation to auditors at any time.
The third mistake is thinking that “medical grade” is a one-size-fits-all label. The FDA and other regulators don’t have a specific definition of a “medical capper”—they define a capping process that meets specific requirements for your product. A machine that works for packaging diagnostic test strips might not work for implantable pacemaker leads, because the sterility and seal requirements are entirely different. That’s why it’s so important to work with a supplier who understands both capping technology and the nuances of medical device regulations, not just a supplier who sells “medical equipment” as a buzzword.
Now, I know there are still skeptics out there. I’ve had quality directors walk out of my demos because they think a capping machine is just a capping machine, and anything less than a custom-built device is a risk. I get it—your job is to keep patients safe, and a failed seal or a contaminated device can have life-threatening consequences. That’s why I always tell them: bring your product, bring your specs, bring your regulatory requirements, and we’ll run a free, no-obligation test batch for you. We have a lab in our headquarters where we can test seal integrity, torque consistency, material compatibility, and even run simulated audits to make sure our machine meets your needs. No sales pitch, no pressure, just real data.
At the end of the day, the question “Can a capping machine be used for medical device packaging?” has a clear answer: yes, if it’s modified and validated to meet the specific requirements of your medical device. It’s not about buying a whole new technology—it’s about adapting proven capping technology to the strict standards that come with medical products. I’ve seen it work for startups, for mid-sized manufacturers, even for large pharmaceutical companies that wanted to upgrade their packaging lines without downtime or huge costs.
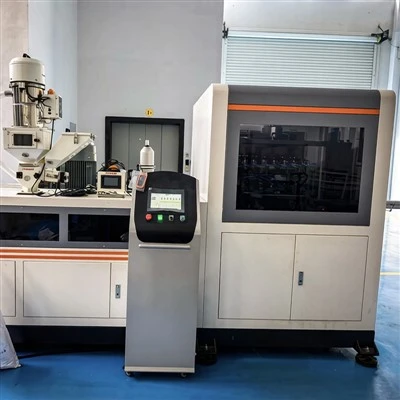
If you’re a medical device manufacturer who’s been struggling to figure out if your current capping setup works, or if you’re looking to upgrade your line and avoid the pitfalls of custom machines, I’d encourage you to reach out. We’ve helped hundreds of clients across the medical device industry, from single-use diagnostic tools to implantable devices, and we can help you find a solution that fits your needs, your budget, and your regulatory requirements. Whether you need a small semi-automatic machine for a startup lab or a full inline line for a large-scale production facility, we can tailor our capping technology to work for you. Don’t let the fear of non-compliance or the pressure of a tight launch timeline derail your product—let’s talk about how a modified capping machine can get your medical device to market safely and on time.
Cap Mold References
- U.S. Food and Drug Administration. (2023). Guidance for Industry: Packaging and Labeling for Human Medical Devices.
- International Organization for Standardization. (2016). ISO 13485: Medical Devices – Quality Management Systems – Requirements for Regulatory Purposes.
- European Medicines Agency. (2022). Guideline on Good Manufacturing Practices (GMP) for Medicinal Products for Human Use, Annex 11: Computerised Systems.
- American Society for Testing and Materials. (2021). ASTM F88: Standard Test Method for Seal Strength of Flexible Barrier Materials.
- International Organization for Standardization. (2019). ISO 14644-1: Cleanrooms and Associated Controlled Environments – Part 1: Classification of Air Cleanliness by Particle Concentration.
Taizhou Koni Mould Co., Ltd.
As one of the most professional capping machine manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale high quality capping machine made in China here from our factory. For pricelist, contact us now.
Address: No. 97 Jinju Road, Chengjiang Subdistrict, Huangyan District, Taizhou City, Zhejiang Province
E-mail: kn@kenimould.com
WebSite: https://www.kenimouid.com/
